

 Home » Applications »
Cutting Tools for Mixed-Material and Short-Batch Machining
Help your customers handle changing jobs, mixed materials and smaller batches by reviewing the current tool, workpiece and setup before narrowing down the alternatives worth testing.
 Discuss a Customer Application
Start With the Job in Front of You
General engineering may involve a one-off repair part, a short production run or a repeating job in a different material. The useful starting point is the current component and process—not a long list of possible tools.
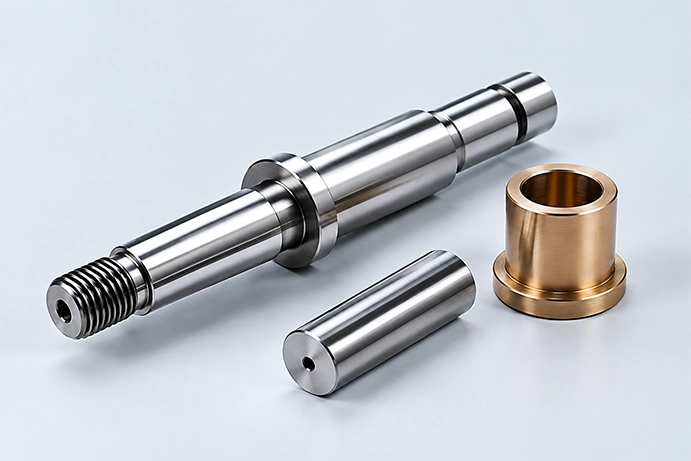
Shafts, Pins & Bushings
Common operations: Turning, Grooving, Drilling, Boring
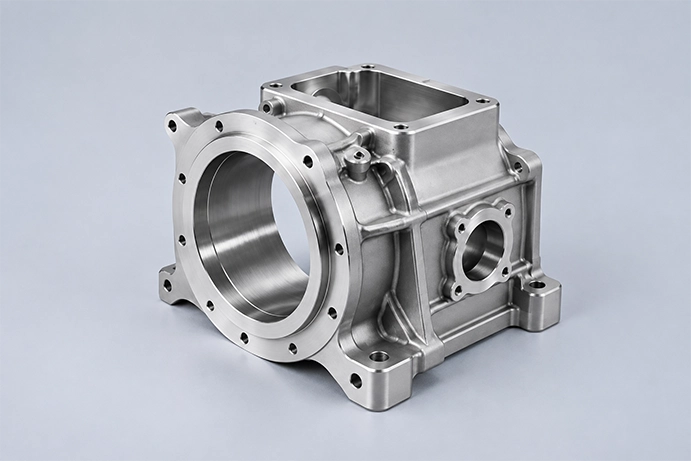
Housings, Flanges & Covers
Common operations: Turning, Grooving, Drilling, Boring
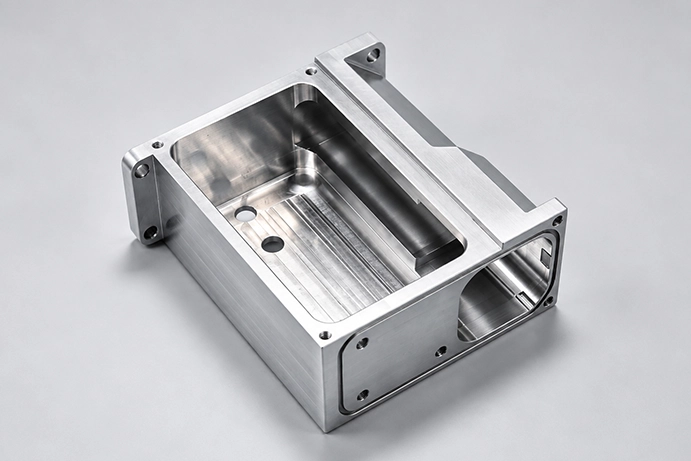
Fixtures, Repair & One-Off Parts
Common operations: Turning, Grooving, Drilling, Boring
What Usually Changes From One Job to the Next
Material Changes
Check First:
Material group, hardness and surface condition.
Why It Matters:
Steel, stainless steel, cast iron and aluminum do not create the same wear or chip behaviour.
Short Batches & Changeovers
Check First:
Batch size, repeat frequency and setup time.
Why It Matters:
A highly specialised tool may not earn its place when the job changes frequently.
Chip Control
Check First:
Operation, depth of cut, feed and available chip space.
Why It Matters:
Unstable chips can interrupt production even when tool life appears acceptable.
Setup & Rigidity
Check First:
Holder interface, overhang, workholding and machine condition.
Why It Matters:
A grade change cannot correct vibration or weak support in the setup.
Materials and Tooling Considerations
Different engineering materials create different wear, chip-control and setup requirements. Start with the material and operation before narrowing down the tooling option.
| Material | Typical Parts | Common Operations | What to Confirm |
|---|---|---|---|
| Carbon & Alloy Steel | Shafts, pins, flanges, fasteners | Turning, grooving, drilling | Hardness, scale, depth of cut, rigidity |
| Stainless Steel | Bushings, fittings, small housings | Turning, milling, drilling | Work hardening, coolant, chip evacuation |
| Cast Iron | Housings, covers, machine parts | Turning, facing, milling | Grade, inclusions, interrupted surfaces |
| Aluminum Alloys | Fixtures, covers, light housings | Milling, drilling, boring | Alloy type, built-up edge, chip evacuation |
Application Note: Exact cutting data depends on tool geometry, grade, holder, machine and job conditions.
Relevant Tool Families
Use these links to understand the available range. For a specific alternative, start with the current tool and application rather than choosing only by appearance.
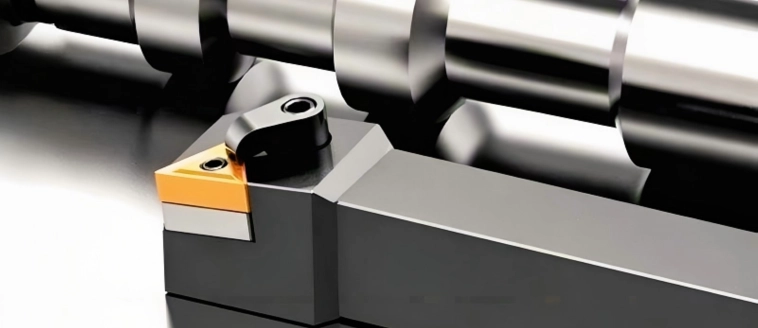
Turning & Boring Inserts
Options for external turning, internal turning and boring across common engineering materials.
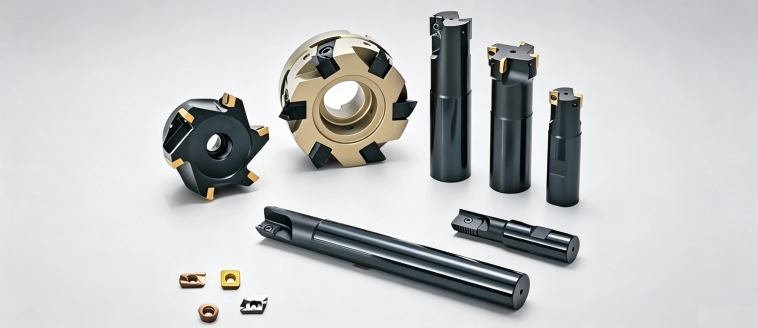
Milling Inserts & Cutters
Indexable milling options for faces, shoulders, slots and general component work.
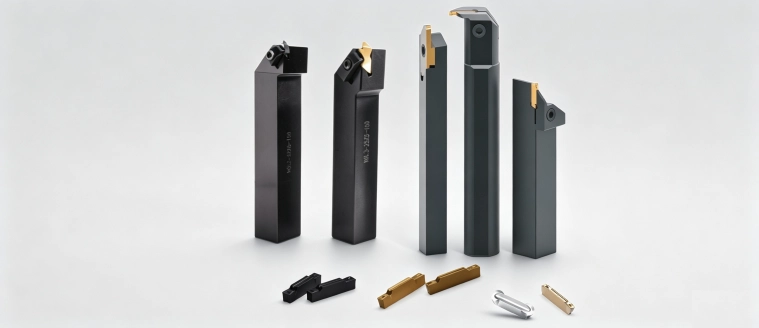
Grooving & Parting Tools
Insert and holder combinations for grooves, parting and profile features.
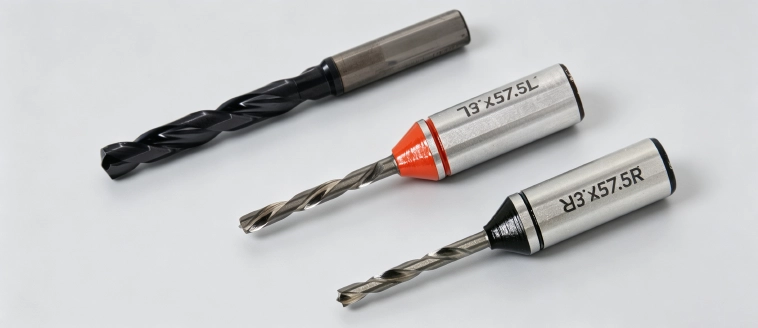
Solid Carbide Drills
Drilling options organised by diameter, depth, material and hole requirement.
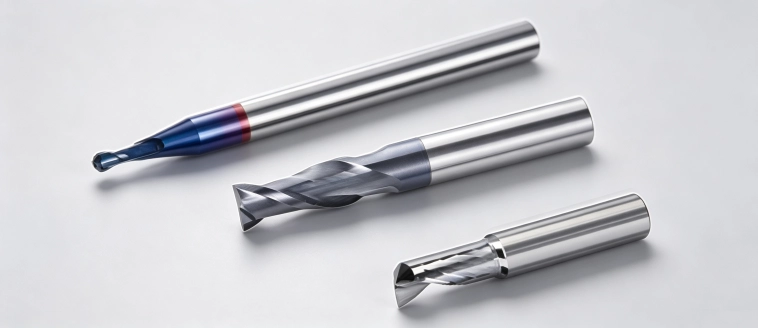
Solid Carbide End Mills
General milling tools for slots, profiles, pockets and finishing operations.
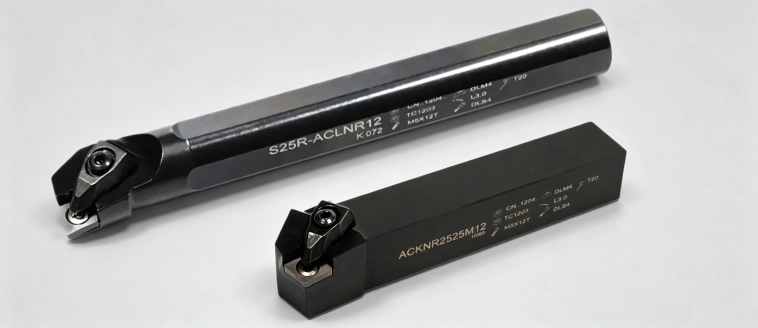
Toolholders & Boring Bars
Supporting holders, bars and cutters to complete the tooling setup.
Your Attractive Heading
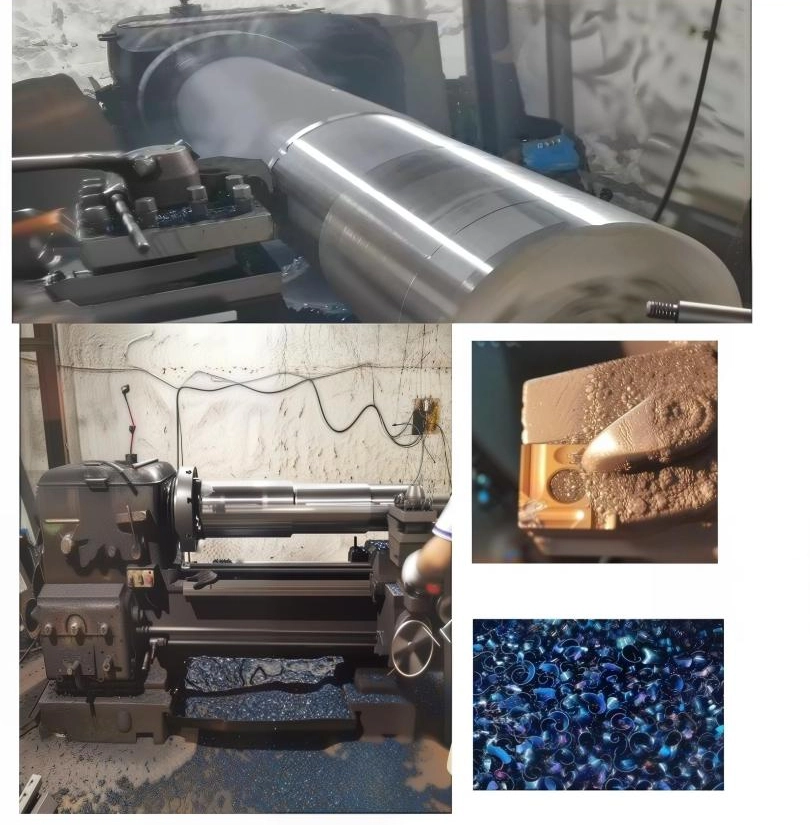
Matched Baseline Performance in 38CrMoAlA Injection-Screw Turning
Same Parameters · Same Recorded Output · Comparable Performance
🔸Material: 38CrMoAlA · HRC30
🔸Operation: Semi-Finish and Rough Turning · Interrupted Cut
| Competitor Baseline | Premitools Test | |
|---|---|---|
| Carbide Insert | SNMG120404-R-S | SNMG120404-R-S |
| Grade | Competitor | TP9325 |
| Cutting Speed | 140 m/min | 140 m/min |
| Feed Rate | 0.40 mm/r | 0.40 mm/r |
| Depth of Cut | 6.5 mm | 6.5 mm |
| Recorded Result | 14 groove sequences | 14 groove sequences |
Under the same cutting conditions, the Premitools insert completed 14 groove sequences and matched the recorded performance of the competitor insert.
How We Help You Evaluate Another Option
A cross-reference is only the starting point. The current job decides what is worth testing.

01 Review the Current Job
-
Start by understanding the existing machining application, including the current tool, workpiece material, machining operation, machine condition and expected performance target. These details help define the actual requirement before evaluating any alternative tooling option.

02 Narrow Down the Options
-
Based on the application requirements, we identify the tooling combinations that are most relevant for a controlled comparison. The evaluation focuses on suitable tool geometries, grades and configurations instead of testing unrelated options.
03 Record the Trial Result
-
After testing the selected option, the results are reviewed based on practical machining factors such as tool life, chip control, part quality and repeatability. Recording these results helps determine whether the proposed solution delivers consistent performance for future applications.
FAQs
-
How do I start if the customer’s jobs change frequently?

-
Start with one current job rather than the complete tooling list. Share the tool code or drawing, material, operation, machine and the result that needs to improve. This gives enough context to identify a controlled first trial.
-
Can one carbide insert grade cover every material?
-
No single grade or geometry is the best choice for every material and operation. Some options can cover a useful working range, but steel, stainless steel, cast iron and aluminum still require different checks for edge strength, coating, chip control and built-up edge.
-
What information helps you recommend a better alternative?
-
The most useful details are the current tool code, workpiece material and hardness, operation, machine or holder, cutting conditions and the current problem. A component photo or drawing is also helpful when the operation is not obvious.
-
Can we test a small quantity before adding a new tool line?
-
Yes. A small controlled trial can be used to compare the proposed option with the current tool under the same recorded conditions. Availability and trial quantity depend on the item.
-
Do you also supply toolholders and boring bars?
-
Yes. Supporting holders, boring bars and milling cutters can be reviewed together with the insert or drilling requirement. The holder interface and setup still need to be confirmed before supply.
Have a Current Job to Evaluate?
Send the current tool code and brief application details. We will review the material, operation and what needs to improve before suggesting a practical next step.


